Home › Integrated Engineering Solutions › HALT Testing

Field Failures Find The Weak Spots Your Testing Never Did

Reliability Engineering Services That Find Weak Points Before Launch

On designs we engineer: we plan HALT, a partner lab runs it, we fix what fails

Find the weak points before launch. Free assessment and roadmap.

Is This Your Problem?

Signs You Need Reliability Engineering Services Now

Reliability Testing Gaps: Field Returns, Claims, And Unknown Margin

Your product passes its qualification tests, then fails in the field. Qualification tests check that a design meets a spec. They don't show how far it is from failure, or which part gives out first. Our reliability engineering services answer that with HALT testing (highly accelerated life testing). A partner lab pushes prototypes past their limits with stepped heat, cold, and vibration. If nothing changes, the field finds the weak points for you, after the design is frozen and tooling is paid for. We find them early, fix the root cause in the design, and retest.

If nothing changes, the field finds the weak points for you. Warranty claims, returns, and recalls cost far more than a test program, and they cost trust you can't buy back. Each failure arrives late, when the design is frozen and tooling is paid for.

PPS HALT testing finds the weakest links early. Engineers analyze each failure, fix the root cause in the design, and retest, so the product gains margin before launch. Reliability testing becomes a design tool, not a pass/fail gate.
✓

Field returns keep coming back

Units that passed qualification fail in customers' hands.

✓

Warranty costs are climbing

Each claim costs parts, labor, and goodwill.

✓

Nobody knows the real margin

The design passes spec, but no one knows how close it is to failing.

✓

Failures we can't reproduce

Nobody owns product failure root cause engineering. Faults come and go and show up only in the field.

✓

A launch with no room for surprises

Late failures push the schedule and the budget.

✓

Qualification tests are all we run

Pass/fail tests don't show where the design will break.

The Usual Fix vs. Ours

Why Pass/Fail Tests Miss What Our HALT Testing Finds

The Usual Test Checks The Spec; Ours Finds Where The Design Breaks

Common approach

Test to spec and ship

Outdated
  1. Run qualification tests

    Pass or fail against the spec

  2. Ship when it passes

    No idea how much margin is left

  3. Wait for field data

    Customers find the weak points

  4. Fix after launch Rework

    Recalls and warranty eat the margin

Failures arrive late
Cost returns as returns, claims, and recalls
PPS approach

HALT on the design

Recommended
  1. Step-stress the prototype

    Heat, cold, and vibration past spec

  2. Find the first failure

    See which part gives out first

  3. Fix the root cause

    Change the design, not the test

  4. Retest and confirm

    Margin shown before launch

A product with real margin
A product with real margin, and the test data to show it
Proof

Reliability Engineering Services Backed By Public Proof

Design For Reliability: What One HALT Fix Did For A Satellite Maker

34%
Less Rework
PPS Innovation Edge white paper
51%
Fewer Prototypes
Source: PPS Innovation Edge white paper
37%
Shorter Test Phase
PPS Innovation Edge white paper

The 34% less rework, 51% fewer prototypes, and 37% shorter test phase figures are from the PPS Innovation Edge white paper.

Public benchmark

HALT Found It; A No-Cost Fix Held

50 °C

Margin added by one fix

Precedent

A satellite maker's HALT fix added 50 °C of margin; the flaw never recurred in 95 units (SS/L, 2012).

What it means

HALT finds the weak point on the bench, not in the field. We plan HALT on designs we engineer, a partner lab runs it, and we make the fix.

HALT Program at Space Systems/Loral, Aerospace Testing Seminar, 2012

What Changes For You

How Reliability Engineering Services Lower Product Cost

Mechanical Testing Services Turned Into Design Levers You Can Use

Lever

Decision it lets you make

Result

Thermal

Parts that fail hot or cold

Decision

Step-stress finds the temperature where each part stops working.

→

Result

Margin on both ends of the range. FEA thermal analysis →

Vibration

Cracks and loose joints

Decision

Rising vibration finds the joints, welds, and fasteners that fail first.

→

Result

Joints that hold in service. Vibration analysis services →

Root cause

Failures fixed twice

Decision

Each failure is traced to its cause before anything changes.

→

Result

Fixes that stay fixed. Research and development →

Design

Late, costly changes

Decision

Weak points fixed while the design can still change cheaply.

→

Result

Fewer prototype loops. Prototype development →

What You Get

What You Get From Our Reliability Engineering Services

A Lower-Cost Design, The Cost Model Behind It, Your IP, And Support

01

The Design You Needed

A design with more margin: the weak points found, fixed, and retested, with every change shown in CAD.

02

The Data Behind It

Test results and failure analysis you review and approve at each gate, before anything moves to production.

03

The IP Is Yours

You own the IP by default. When an OEM or partner manufacturer is involved, the contract spells out who owns what.

04

Support After Delivery

If we missed it in our QC, we fix it. If your supplier can't make the part within three years, or supply dries up, we fix that too.

You send

What we need to start

Prototypes or early production units

Specifications: operating range, life, and standards

CAD and drawings for the design under test

Field data: returns, warranty, or known failures

Targets: margin, life, or launch date

→

You get

What you hold at the end

A test report with every failure and its root cause

Design changes that fix each weak point

Retest data showing the margin gained

Updated CAD and drawings ready to build

A roadmap for the next round, and a team that stays

We price to the value we deliver, not the hours we log. If the value isn't there for you, we'll say so in the assessment.

Bring your own test lab, or work with the partner labs in our network. A partner lab runs the chambers. Our engineers plan the test, read every failure, and make the fix.

How We Work · HALT Testing

How Our Reliability Engineering Services Find Weak Points

From Your Prototype To A Proven Design You Approve At Each Gate

01
Assess
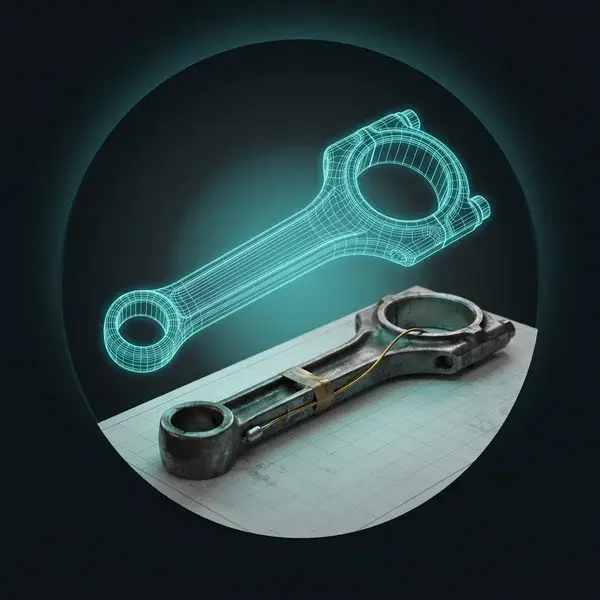
Wireframe of a connecting rod over a spec sheet by a worn field unit: the start of reliability engineering services for you
We review your project scope, design, and specs, and agree which lab runs the test.
02
Roadmap
Stepped line climbing a dark disc from frost blue to warm amber with gates: the HALT plan in reliability engineering services
Test plan, stress steps, and the gates where you decide.
03
Test
Connecting rod on a vibration table, half frosted and half warm, a gold glint at a crack: HALT in reliability engineering
A partner lab runs the step-stress test; we find each failure and its cause.
04
Fix
FEA of the redesigned connecting rod, a smoother blend at the small eye now low stress: the fix from reliability engineering
Design fixes, retest, and updated CAD and drawings.
05
Support
Connecting rod on a crankshaft with a gold vibration sensor on its bearing block as reliability engineering tracks field data
Production questions, field data, and changes.

You approve every test plan, design change, and its cost at every gate, so nothing that affects function surprises you. If we missed something in our QC, we fix it. If a supplier can’t make the part within three years, we fix that for you too.

Every field failure costs more than the test. Free roadmap.

Get Your Free Roadmap
Where We Solve It

Reliability Engineering Services Across Your Industry

The Same Weak Points In Aerospace, Automotive, Mining, And Power

Aerospace And Defense

Housings, brackets, and harnesses stepped past flight limits so weak links show on the bench, not in use.

Margin you can measure.

Applications

Fittings

Housings

Explore Aerospace Work

Automotive And Mobility

Modules, mounts, and assemblies pushed past road and climate limits before the vehicle program locks.

Fewer warranty claims.

Applications

Housings

Assemblies

Explore Automotive

Mining Equipment Makers

Machines and enclosures that run in heat, dust, and impact, tested to failure before they go underground.

Stop costly downtime.

Applications

Frames

Wear Parts

See Mining Equipment

Power Generation Systems

Plant hardware and enclosures stressed past their ratings, so failures surface before an outage does.

Fewer forced outages.

Applications

Fittings

Fabrication

See Power Gen Work
Related Solutions

Solutions Related To Reliability Engineering Services

Prototype And R&D Solutions That Pair With Reliability Work

Prototype Development

We design the prototype, manage the build through partner shops, and test it before you commit to tooling.

Design, build and test.

Applications

Design

Partner Builds

Testing

See Prototype Design

Research And Development

Turn problems and test failures into better designs: root cause, new concepts, and proof that they work.

Fix it at the source.

Applications

Fixtures

Uptime

See Our R&D Services

Every Solution We Offer

Prototyping, HALT, R&D, reverse engineering, and more. See every problem our engineering team solves.

Find your problem here.

Solutions

Prototyping

HALT

R&D

See All Solutions
Why PPS

Why Buyers Choose PPS For Reliability Engineering Services

A Team That Proves Every Fix With Reliability Testing Data

A Team, Not One Hire

FEA, CFD, CAD, DFMA, and testing under one roof. Engineering is a team sport, and you get the whole team.

One team, every skill.

Under One Roof

FEA

CFD

CAD

DFMA

Testing

Meet Our Engineers

SDVOSB Set-Aside Ready

Veteran-owned SDVOSB status gives defense and federal buyers a set-aside path to proven engineering.

Verify our SDVOSB status.

Credentials

SDVOSB

VOSB

CAGE 8ZK73

NAICS 541330

Verify SDVOSB Status

We Stand Behind It

Missed something in our QC? We fix it. Supplier can't make the part within three years? We fix that too.

Support for the long run.

We Fix

Our QC Misses

Supplier Gaps

Supply Chain

See How Clients Stay

Solutions, Not Hours

We price to the value we deliver, not hours logged. You buy a design that works, not more iterations.

Pay for the result only.

Collections

Gold

Platinum

Diamond

View Pricing Plans
FAQ

Reliability Engineering Services Questions, Answered

Straight Answers On HALT Testing, Data, IP, Results, And Price

How is HALT testing different from qualification testing?

HALT Finds Where It Breaks; Spec Tests Only Show It Passes

HALT testing and qualification testing answer different questions. Qualification checks that a design meets its written spec, and the result is pass or fail. In our reliability engineering services, HALT pushes prototypes well past the spec until something fails, so you learn exactly where the design breaks. A pass tells you the design met the spec on test day. It doesn't tell you how much margin is left, or which part will fail first in service. The NIST/SEMATECH e-Handbook explains how testing at higher stress brings out failures sooner. Without that, the field finds your weak points after launch, when every fix costs more.

A partner lab runs stepped heat, cold, rapid thermal change, and rising vibration. Our engineers find the weakest link, trace its root cause, and fix it in the design. Then the test pushes again to find the next one. Qualification then runs on a design that already has margin. HALT doesn't replace the tests your customer or regulator requires. The free assessment shows where it fits your program.

What do we get from a HALT program?

Failure Modes, Root Causes, And Design Fixes You Can Act On

Our reliability engineering services give you more than a list of failures. For each failure, you get the stress level where it happened, the root cause, and a design change that fixes it. We retest after each fix, so you can see the margin gained at every step. A summary that says a unit failed is not enough. Your team needs to know why, at what stress, and what changed. The DoD's Electronic Reliability Design Handbook covers reliability as part of design, not just test. Without the root cause, the same failure comes back in the next build. Weak units then reach customers.

You also get the operating and destruct limits of your design. Those limits set the screens for production, so weak units are caught before they ship. If a failure points to a supplier part, we tell you which part and why. A partner lab runs the chambers. Your design changes come back as updated CAD and drawings. You own the IP by default, set in your contract.

Can PPS work with our manufacturer or test lab?

Bring Your Own Manufacturer or Lab, or Work With Our Network

Yes. Our reliability engineering services work with the test labs you already trust, or with the partner labs in our network. Many projects use both. What matters is that one engineering team coordinates them, so the builder and the lab always work from the latest released design and data.

When every vendor reports to you separately, you become the integrator. Design changes travel by email, parts get cut to old drawings, and test results arrive without anyone tasked to act on them. The Department of Defense's IPPD Handbook organizes programs around integrated product teams for this reason, with design, manufacturing and test under one shared plan.

PPS manages your builders and test labs inside one engineering loop. We release the design, track every build and test, read the results and make the fix ourselves. Data and NDAs are set up between all parties at the start. You decide how far we take the design, up to the start of production. The IP is yours by default, as set in your contract.

What do you need from us to start?

Send Your Data And Targets; We Build The Roadmap From There

To start a project with our HALT testing, send what you have, in any format. That usually means prototypes or early production units, and the specifications for operating range, life, and standards. Add CAD and drawings, field return or warranty data, and your targets for margin or launch date. Photos of failed parts help us too. Missing data is the most common reason engineering projects stall, because a model built on guessed inputs gives a guessed answer. That is why we don't start the work until every data set is in.

Once it is, the first step is a free assessment of your project scope. We confirm what the work can and can't answer, and tell you what is still missing. Then we send a roadmap proposal with scope, targets, and approval gates. Every project is scoped on its own, so the roadmap sets the schedule, not a stock promise. NDAs are available before you share any files. For gaps in material data, NIST material measurement data is a good first stop.

Who owns the design and the models?

The Design And Models Are Yours By Default, Set In Your Contract

You own the design, the drawings, and the models from your HALT testing project by default, as set in the contract. When an OEM or partner manufacturer is involved, the contract spells out who owns what. Some firms keep the models, or license them back to you, so every later change sends you back to them. That locks your product to one vendor and makes design reviews harder, because your team can't open the evidence behind the decisions. You receive the native CAD, the drawings, the simulation model files, and the documented results. Your engineers can then check the work, rerun a load case, or hand the package to a supplier or customer.

We sign mutual NDAs before any of your data is shared, and your files stay in our controlled project folders while we work. If your program has export-control or customer data rules, tell us at the start and we will set up the data handling to match them. For defense programs, the State Department ITAR guidance sets the rules we follow.

What happens if the design still fails after a fix?

If We Missed It In Our QC, We Fix It; Test Data Improves Design

If the design still fails after a fix, we find out why and fix it again. Hard engineering carries unknowns on any project: real loads, material lots, and assembly effects never match a model perfectly. With HALT testing from PPS, you approve the data at each gate. A test result is then checked against predictions you have already seen, not a black box. A failure in test is data. It shows which assumption was wrong: a load, a material property, or a boundary condition. That data improves the model and the design.

When testing is in scope, we plan the test to confirm the margins that matter most. Then we correlate the model to the results, following ASME verification and validation practice. If the miss was ours, because something slipped through our QC review, we fix it. If the test uncovers a condition nobody knew about, we scope the change with you and update the roadmap. Either way, you get a clear answer and a path to a design that holds.

How is HALT testing priced?

Priced To The Value We Deliver, Never To The Hours We Log

We price every HALT testing program to the value it delivers, not the hours we log. Hourly billing rewards extra iterations, so the cheapest quote often becomes the most expensive project once tooling, rework, and field failures show up. Our incentive is to get the design right the first time. We engage by fit, not as a ladder. Gold (from $35K): you have one project and need help with it. Platinum (from $15K/mo): you have recurring work at a steady rhythm. Diamond (from $800K/yr): you have a long development program, often multi-year.

Gold is never required, and some clients start at Platinum or Diamond. These are starting points, not quotes; your roadmap sets the price. We price to the value we deliver, not the hours we log. If the value isn't there for you, we'll say so in the assessment. Our engineering consultant pricing page explains how each collection works in more detail.

Worried about field failures? Send the design. Free roadmap.

Free Project Scope Assessment. No Obligation. NDAs Available.

Find Weak Points Early With Reliability Engineering Services

Leave With A HALT Test Plan That Targets Your Weak Points First

Send your design, specs, and field data. We review your project scope in a free assessment and reply within one business day with next steps.

SDVOSB Certified
VOSB Certified
CAGE 8ZK73
NAICS 541330

On-site assessments that require travel are quoted separately.